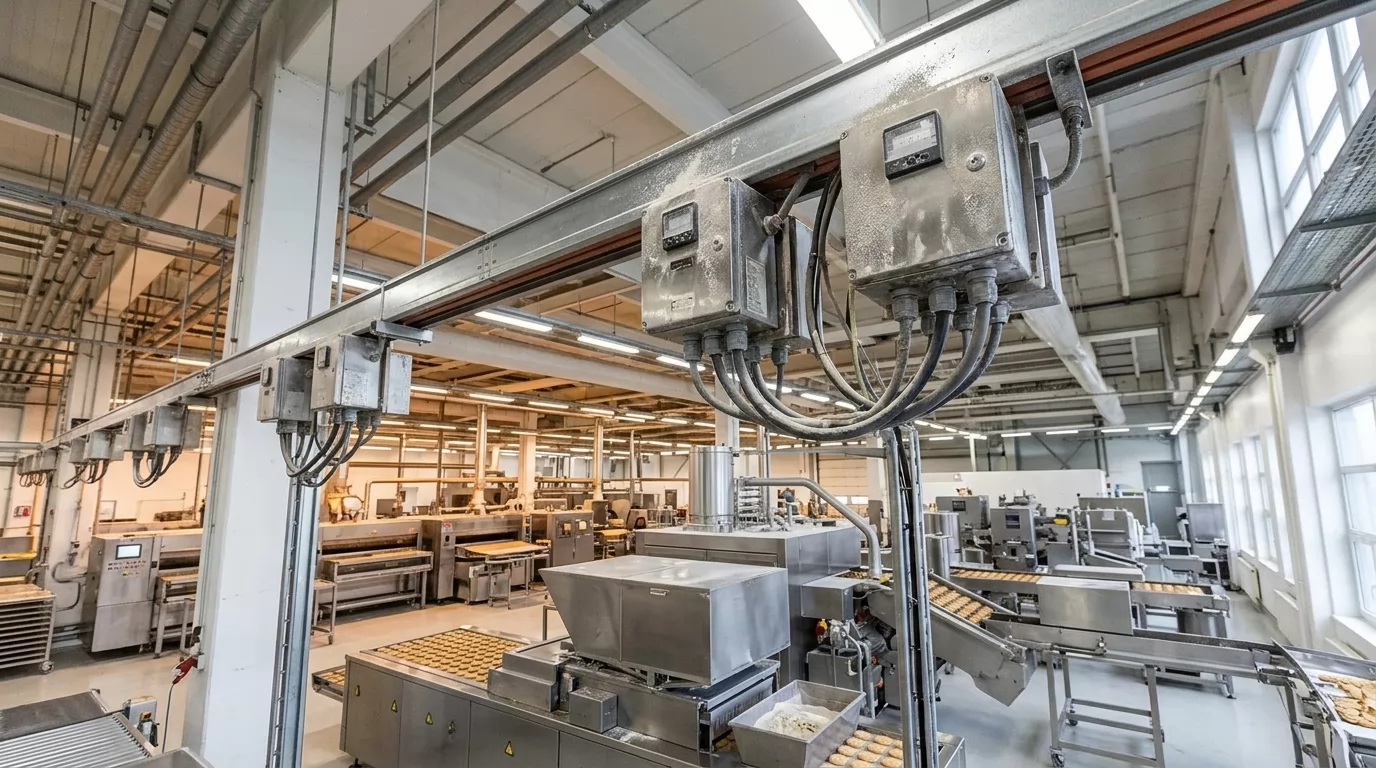
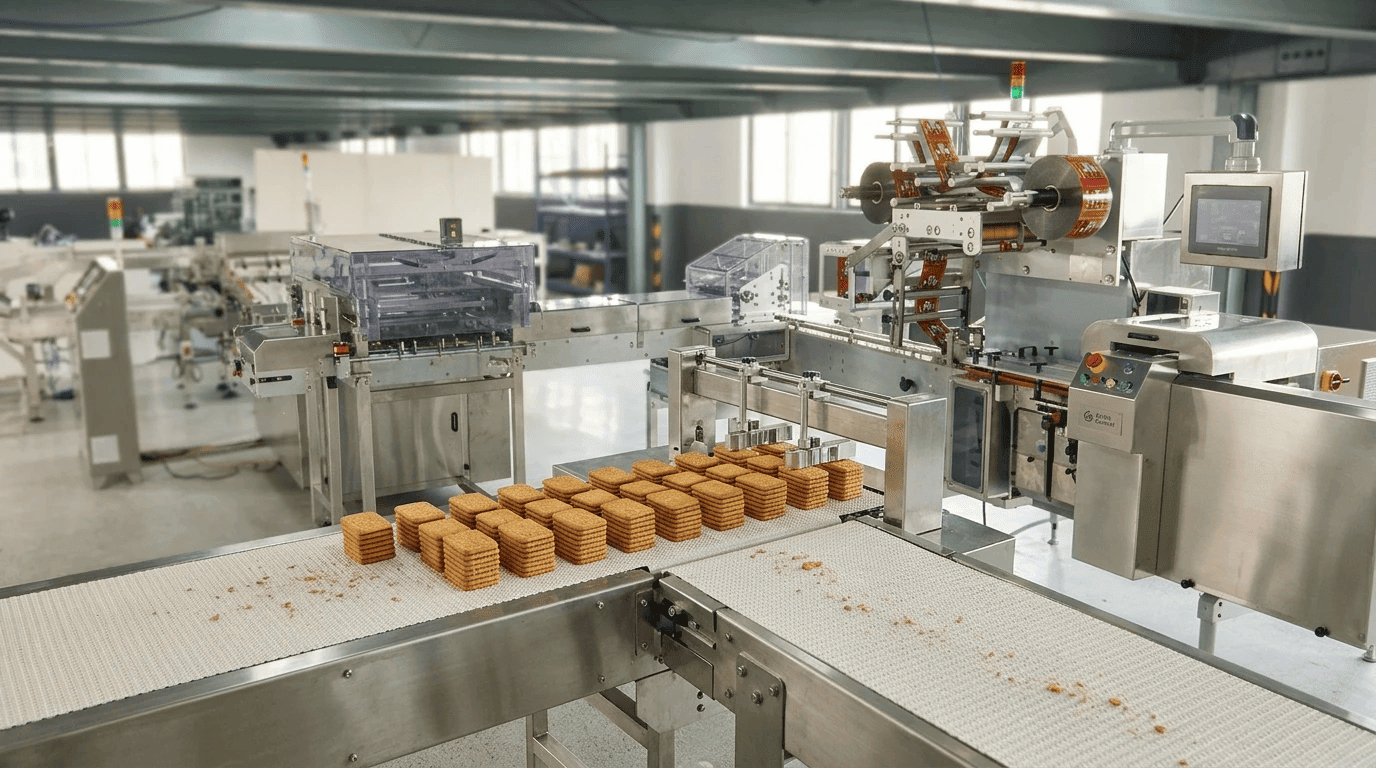
Can a Cake Machine Be Fitted With a Cookie Extruder and Wire Cutting Function?

The decision comes down to four questions: what dough you run, whether the drive and hopper can push it, how the product gets cut, and what the retrofit costs against a dedicated machine. A cake machine cookie extruder conversion is sometimes feasible, but it is rarely a simple bolt-on. This guide is for plant managers and engineers weighing a retrofit against new equipment, and EverSmart is named here only as one of the equipment makers you might put these questions to.
Can a Cake Machine Make Cookies, or Only Batter-Based Products?
Sometimes. So, can cake machine make cookies? It can handle soft doughs and thick pastes, but it rarely copes with stiff shortbread-type doughs unless the pump, hopper and drive are substantially changed.
Three conditions decide it. Run them in order, because a failure at the first usually makes the other two irrelevant.
Dough consistency. A cake depositor is designed around pourable or semi-fluid mass that flows under its own weight and fills a piston chamber. Soft drop-cookie doughs with high moisture and fat can sometimes be pushed through the same path. Dense, low-moisture doughs resist flow, bridge in the hopper and starve the pump.
Pressure and drive capacity. Extruding dough through a die takes far more force than depositing batter through a nozzle. If the motor, gearbox and pump seals were sized for batter, the dough can stall them or wear them quickly. Ask what the drive was specified for, not what it happens to do on a light day.
Cutting and portion control. Batter is cut off by valve closure and a clean nozzle break. Dough needs a defined cut, usually a tensioned wire or a knife, timed to the extrusion stroke. If the machine has no way to coordinate that, weights will drift.
A rule of thumb: if your dough holds a shape on a spoon and still flows slowly, a trial is worthwhile. If it crumbles when pressed, plan for a dedicated machine.
Why Cake Depositors and Cookie Extruders Are Built Differently
A cake depositor is designed to meter a fluid, while a cookie extruder is designed to push a solid-like mass through a restriction and cut it cleanly. That is why any attempt to convert cake depositor to cookie production deserves a closer look: the two jobs look similar on a line diagram, yet the mechanics behind them differ in almost every part that touches the product.
It helps to be clear about the meaning of extruder here. An extruder is a machine that forces a material through a shaped opening under pressure, so the opening defines the cross-section of what comes out. A batter depositor meters a dose; an extruder shapes a continuous mass. That difference in purpose explains most of the design gaps below.
Batter versus dough: what the machine sees
Cake batter is pourable and low in viscosity. It flows under its own weight, so a piston or pump can fill a cavity and a valve can shut off the stream with little resistance. Volumetric dosing works because the material self-levels and refills the chamber without help.
Shortbread dough rheology is a different problem. A fat-rich, low-moisture dough has a meaningful yield stress, meaning it does not move until pressure exceeds a threshold, and it then behaves more like a plastic solid than a liquid. It does not refill a piston chamber by gravity, and it traps air pockets that distort piece weight. Temperature shifts the behavior sharply, because the fat softens or firms with only a few degrees of change.

Where the pressure goes
A cookie extruder spends its pressure budget on feeding. Hoppers are typically shaped to prevent bridging, and feed rolls or augers force dough into the die so the chamber is packed rather than merely filled. The pressure at the die face is what gives each piece a consistent shape and weight.
A standard depositor has none of this. Its hopper relies on gravity, and its piston and valve block are sized for fluid. Put stiff dough through that path and the valve can jam, the piston can stall, or the dough can compact and smear in dead zones. Seals and motors then take loads they were never rated for.
That gap is mechanical, not a matter of settings. It is why any conversion, including a cookie extruder attachment from EverSmart or another maker, has to be assessed against your drive and hopper first, not the nozzle.
Which Cookie Doughs Can a Converted Depositor Handle?
Feasibility depends on how the dough behaves under pressure, not on its name on the recipe card. Four criteria sort most doughs quickly, and they apply the same way whether the attachment comes from EverSmart or any other supplier.
Viscosity and yield stress. Soft, high-moisture drop doughs, such as many chocolate chip or oatmeal-style batters, flow under modest pressure and then hold a mound on the tray. These are the realistic candidates. Stiff, low-moisture shortbread-type doughs resist flow until pressure is high, which a piston-and-valve cake system is not built to deliver.
Fat content and temperature sensitivity. Butter-rich doughs soften with friction and heat inside the hopper and nozzle. A dough that extrudes cleanly at the start of a shift can smear, sag or lose definition an hour later. If your recipe depends on tight temperature control, test it over a full run, not a few minutes.
Inclusion size and load. Chocolate chunks, whole nuts and fruit pieces bridge across narrow orifices and valve seats, causing blockages and uneven piece weight. As a rule of thumb, inclusions should be well under the orifice diameter, and heavy loads usually push a recipe out of reach for a converted unit.
Shape expectation. Drop and simple piped shapes suit a depositor. Sharp-edged, patterned or wire-cut pieces rely on a firmer dough and a defined cut, which a retrofit seldom reproduces well.
Soft drop doughs and some piped doughs are worth trialing. Stiff, dry or inclusion-heavy doughs are better left to a dedicated machine.
What Does a Cake Machine Cookie Extruder Actually Involve?
A cookie extruder attachment for cake machine setups is a set of parts that lets a depositor push dough through a shaped die and cut it into pieces. It is a chain of changes, not one add-on. Work through it in this order.
Replace the hopper or feed section. A batter hopper relies on gravity. Dough needs a feed mechanism, usually twin rolls or an auger, that forces material into the pump or cylinder without bridging.
Rework the pumping stage. The piston and valve block that meter batter may stall or leak under dough pressure. Expect a different pump, a reinforced cylinder, or both.
Fit a nozzle plate or wire-cut die. The die sets orifice size and profile. Its seat must match the manifold, and the plate must withstand higher back pressure than a batter nozzle sees.
Add the cutting mechanism. A tensioned wire, or a cutting blade, separates each piece at the die face. Its motion has to be timed to the extrusion stroke, so it needs its own drive and guarding.
Change the drive and controls. Stiffer dough asks for more torque. Many conversions need a larger motor, a servo-driven extrusion axis, and new recipe parameters for stroke, speed and cut timing.
Adapt the conveying and cleaning set-up. Trays or belts must suit the new piece spacing, and the dough-contact parts need to come apart for washdown.
Steps 1, 2 and 5 are where most retrofits grow in cost. Treat the die and cutter as the easy part.
That is why a conversion is rarely a bolt-on. If you ask a supplier such as EverSmart, or the original manufacturer, to scope it, request the list above itemized, so you can see which parts are new, which are modified and which are reused.
How Does Wire Cutting Work, and Can It Be Added to a Depositor?
Picture a line where dough leaves the die in a steady ribbon and a thin wire sweeps across the face, dropping one piece at a time onto the belt. If the wire is late, pieces run together. If it is early, they come out short. That timing relationship is the whole technique.
Wire cutting is a method in which a tensioned wire travels across the die face and slices the extruded dough free. The wire moves in a straight or slightly curved path, usually driven by a pneumatic cylinder, a servo axis or a cam linked to the extrusion stroke. Because the cut happens at the die, piece length is set by how far the dough has advanced before the wire passes, not by the nozzle alone.

Can a depositor take one? Often, yes, provided the machine has a controllable extrusion stroke and an input that can trigger or follow the cutter. A depositor with a fixed mechanical cycle and no controller access is a poor candidate, since the wire cannot be synchronized with dough flow.
Mounting and travel path
The wire frame must sit directly against the die face with a small, consistent gap. Too wide and dough smears behind the wire. Too tight and the wire drags on the plate. Check that the nozzle plate is flat and rigidly held, because any flex shows up as uneven cut lengths. Allow clear travel on both sides of the die, which can be a problem on compact depositor heads.
Cleaning access
Wires foul with fat and dough residue, so the frame should come off without tools, and the wire should be replaceable in minutes. Ask whether the mounting leaves dead pockets where dough can pack in. When EverSmart or any other supplier quotes the cutter, ask for the frame, tensioning method and guarding to be shown together, since the sweep zone is also a pinch hazard.
Wire-Cut Versus Depositing: Which Fits Your Product?
Depositing pushes a measured mass of dough or thick paste out of a nozzle and lets it drop or be wiped off, while wire cutting extrudes a continuous ribbon and slices it at the die face. Depositing is simpler and forgiving on soft, wet doughs. Wire cutting gives cleaner edges and better portion control on firmer doughs, but it asks more of the drive and the cutter timing.
| Method | Suited dough | Shape and edge definition | Weight consistency | Changeover effort | Typical limits |
|---|---|---|---|---|---|
| Depositing | Soft, high-moisture drop doughs; thick pastes | Rounded, softer edges; tails and spread are common | Good on uniform doughs; depends on dosing stroke | Lower: nozzle and hopper swaps | Struggles with stiff doughs and larger inclusions |
| Wire cutting | Medium to firm doughs, including many shortbread-type recipes | Sharper edges; pattern follows the die profile | Good when extrusion pressure and cut timing stay steady | Higher: die, wire frame and cutter settings | Needs adequate drive power; very sticky doughs can drag on the wire |
The takeaway: dough consistency should pick the method before anything else does.
Inclusions deserve a separate thought. Small chips and fine pieces pass through either method, but large inclusions can catch on a wire or clog a small die orifice. Depositing tolerates chunkier mixes when the nozzle is wide enough.
If your range is mostly soft drop cookies at modest volume, a depositor setup is usually enough, and it is the cheaper path to keep. If your core products are firmer doughs with defined shapes, wire cutting is the better fit, and that is where a conversion starts to strain. Ask a supplier such as EverSmart to run your own dough on the method you are considering rather than rely on a generic demonstration.
Is the Drive Strong and Precise Enough? Servo Control and Duty Cycle
The usual failure on a converted depositor shows up a few weeks after commissioning. The first trials look fine, then the motor runs hot, the ribbon starts to pulse, and piece weights drift as the shift goes on. Nine times in ten the cause is a drive sized for batter, now asked to push dough against a die.
Cake programs rarely need much torque. Dough through a restrictive die does, and it needs it continuously, not in short bursts. Check three things before anything else: peak torque at the extrusion shaft, continuous torque at the speed you plan to run, and the thermal limit of the motor and gearbox over a full shift. A drive that copes for twenty minutes in a trial can still be undersized for eight hours.
Precision matters just as much. A servo-driven extrusion axis, which is a motor with closed-loop position and speed feedback, holds a steady dough flow and lets the cutting wire stay synchronized with it. An older pneumatic or open-loop drive may leave you with weight variation you cannot tune out. If the existing machine has servo axes, ask whether the controller can add a cutting axis and store separate recipes for dough.

Gearing is the quieter trap. Reducing speed to raise torque can lower output below your target, so confirm both numbers together at your real piece weight and line rate.
Tip: Ask the OEM for torque and duty-cycle limits in writing, stated for your dough and die, rather than assuming the cake program carries over. EverSmart or any other supplier should be willing to put those figures in the quotation.
If the answer is vague, treat the drive as a replacement item and budget for it.
How Do Dies and Depositor Nozzles Affect Weight and Shape?
Rule of thumb: size the die to the dough, never the dough to the die. The orifice sets the cross-section of the extruded ribbon, so piece weight follows from that area multiplied by the cut length. Get the orifice wrong and no amount of speed adjustment will recover the weight target.
Land length, the straight section just before the exit, matters more than most buyers expect. A longer land builds back-pressure and smooths the flow, which usually gives cleaner edges and steadier weight. It also raises the load on the drive. A short land is easier to push but tends to let the dough swell and tear at the exit.
Shape and spread come from the dough, too. Doughs rich in butter relax after leaving the die and widen on the belt, so the die profile often has to be cut smaller than the finished piece. Fluted or star profiles hold their detail only in doughs with enough body to keep it through the oven.
The rule breaks at one point. If the dough is stiffer than the machine can pump, a new die changes nothing, because the limit sits upstream in the hopper, feed and drive. This is why a nozzle swap alone does not turn a batter machine into a dough machine. EverSmart and other equipment makers can supply dies in several profiles, but the die only shapes what the machine can already deliver.
Before you order, test the actual dough through the proposed die at production temperature. Record piece weight over a sustained run, not a handful of samples.
What Compliance Checks Apply to a Modified Machine?
Does adding a cookie extruder change the machine's legal status? Often, yes. Under the EU Machinery Directive 2006/42/EC, a substantial modification can make whoever carries it out responsible for the conformity of the result. That can mean a fresh risk assessment, updated technical documentation and a new declaration of conformity. Whether your change counts as substantial depends on the details, so ask the original manufacturer and a qualified assessor to decide it in writing. EverSmart, for one, would expect that question before any retrofit drawing is approved.
The cutting zone deserves the closest look. A moving wire at the die face creates a new cutting and entanglement hazard that the cake program never had. Fixed or interlocked guards, safe stopping behaviour and sensible access for cleaning all need to be reviewed against the new configuration, and the control system's safety functions may need rework as well.
Hygiene is the other half. Parts touching dough, including the hopper, die, wire holder and fasteners, should be food-grade stainless steel, commonly grade 304, with smooth welds and no dead pockets where dough can sit. Also check that any seals, gaskets and the wire itself are rated for food contact.
Then fold the new parts into your HACCP plan. Look at cleaning access, allergen changeover between cake and cookie products, and whether the wire or die can be removed and inspected without tools or awkward reach.
Retrofit or Buy a Dedicated Wire-Cut Machine? Cost and Risk Compared
Take a bakery that runs cake cups on one depositor and wants a soft drop cookie for a single customer, a few shifts a week. The dough is close to a thick paste, the order is modest, and the depositor sits idle part of the time. A retrofit makes sense here: a new nozzle plate, a modified hopper and perhaps a drive check cost far less than a second machine.
Now change the brief. The customer wants a shortbread-style dough, tight piece weights and a steady output into an existing cooling conveyor and packing line. The retrofit list grows: feed section, stronger drive, cutting unit, guarding, new controls. Each item is a separate engineering task, and each adds validation time.
The lesson is that purchase price is the wrong yardstick. Total cost of ownership should include engineering hours, trial batches, downtime during conversion, changeover labor between cake and cookie, scrap from weight drift, and the risk that the modified machine never reaches rated speed. A dedicated wire cutting cookie machine carries a higher entry cost but is built and documented for the job, including its conformity file.

EverSmart, as a machinery supplier, would ask you for dough samples and target output before advising either route, and that is a fair test of any vendor. If a supplier quotes a retrofit without seeing your dough, treat the quote as a guess.
Rule of thumb: retrofit for soft dough and low volume; buy dedicated once the dough is stiff or the line must hold tolerances.
How to Choose: Criteria to Settle Before Any Quote
Settle five things in this order, because each one narrows the next. Quotes requested before they are fixed tend to describe different machines and cannot be compared.
1. Dough. Decide the recipe family and its worst case: the stiffest, coldest, most inclusion-heavy version you will run. Everything downstream follows from it, and a vendor can only judge feasibility against a real sample.
2. Target output. State pieces per minute and shifts per week, not "as fast as possible." Low, occasional volume favors a retrofit; sustained output exposes drive and duty-cycle limits.
3. Piece-weight tolerance. Write down the allowable variation per piece and per tray, and who checks it. Tight tolerances usually push you toward servo-driven extrusion and a purpose-built die.
4. Line integration. Confirm belt height, pitch, oven loading and any downstream cooling or packing. A machine that cuts well but cannot hand pieces onto your existing conveyor creates a second project.
5. Floor space. Measure clearance for hopper loading, wire access and cleaning, not only the footprint. EverSmart, like any supplier, can only size a solution against these dimensions.
Rule of thumb: if you cannot fill in the first three in writing, you are not ready to request a quote.
Common Mistakes and Myths About Converting a Cake Depositor to Cookie Production
The most common assumption is that a nozzle swap is enough. It isn't. A new orifice changes the shape of the exit, but the pump, hopper and drive still have to push a dough that behaves nothing like batter. Treat nozzles as the last change, not the first.
"Any dough will extrude." Recipe names mislead here. A butter-rich dough that flows at 22°C can turn stiff and crumbly at 18°C, and heavy inclusions can block a small orifice or tear the ribbon. Define your stiffest, coldest and most inclusion-heavy version, then test that one.
"One successful trial proves every recipe." It proves one recipe, on one day, at one temperature. Each additional dough needs its own run, ideally over a full shift, because weight drift and drive heating show up late.
"The cake program carries over." Torque, duty cycle and stroke timing were sized for batter. Ask EverSmart or any other supplier to confirm limits for dough in writing before you commit.
"Compliance stays unchanged." A new cutting zone can alter the machine's conformity position, so settle that before purchase, not after installation.
FAQ
Can the same machine run both cake and cookies?
Yes, for soft doughs, but expect changeover time. Hopper, die and cutter swaps plus a full clean-down between allergen or product changes are the real cost.
Should the manufacturer do the retrofit?
Yes, ideally. The original maker knows the drive limits and conformity file; if that is not possible, an engineer such as EverSmart can quote the modification, but check who carries responsibility.
How do I trial dough before committing?
Run your stiffest, coldest production recipe on the supplier's test rig. Check piece weight over a sustained run, not a few shots.
Is a nozzle swap enough to make shortbread?
No. Stiff dough needs a different feed and pump stage, and usually a stronger drive.
Conclusion
Convert a cake depositor only when your dough is soft, your volumes are modest, and you have run trials on the worst-case recipe and cleared the compliance review for the cutting zone. If the dough is stiff, the output target is steady, or the machine must sit inside a bakery production line, buy a dedicated wire-cut machine. Before you commit either way, send your stiffest recipe to the original maker or to an engineering firm such as EverSmart and get the torque, duty-cycle and conformity position back in writing.
Ready to start your journey toward a customized solution? Contact me directly on WhatsApp to begin the conversation.